Quantitative
PLATFORM 01
FlowQuant™
Fluorescence quantitative rapid testing platform integrating test strips with multi-channel incubator-readers for efficient on-site and routine screening.

About Xinyu Bio
Xinyu Bio develops and manufactures testing reagents, instruments, sample preparation systems and automated workflows for food safety, animal nutrition and animal health diagnostics.
Who We Are
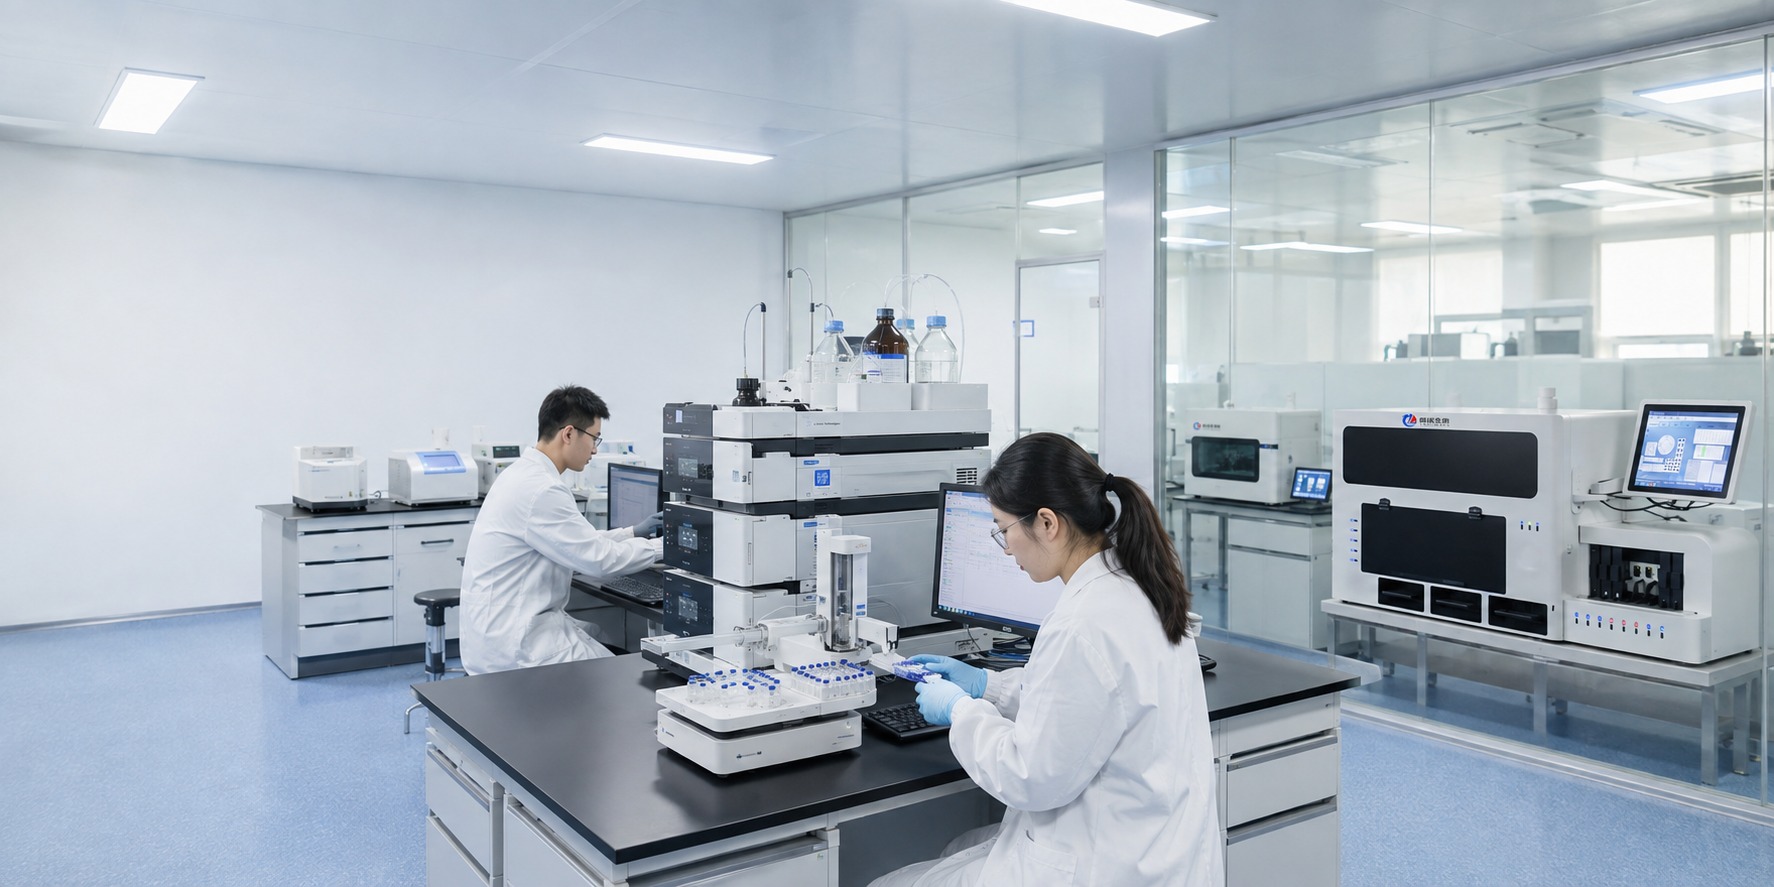
Shandong Xinyu Biotechnology Co., Ltd. is an R&D and manufacturing company developing practical testing technologies for food safety, animal nutrition and animal health diagnostics. From core reagents and assay design to instruments, molecular diagnostics and intelligent automation, our capabilities are organized through four complementary platforms—helping customers build coordinated, repeatable testing workflows.
Fluorescence quantitative rapid testing platform integrating test strips with multi-channel incubator-readers for efficient on-site and routine screening.
High-sensitivity ELISA platform for laboratory-based testing of mycotoxins, veterinary drug residues and soybean anti-nutritional factors.
qPCR molecular diagnostics platform supporting rapid pathogen detection and disease monitoring across aquaculture, poultry, livestock and pets.
Intelligent automation platform covering automated sample preparation, mycotoxin testing, cleanup workflows and integrated laboratory systems.
Our R&D Team
Our multidisciplinary organization connects scientific research, product engineering, manufacturing, quality control and application support.
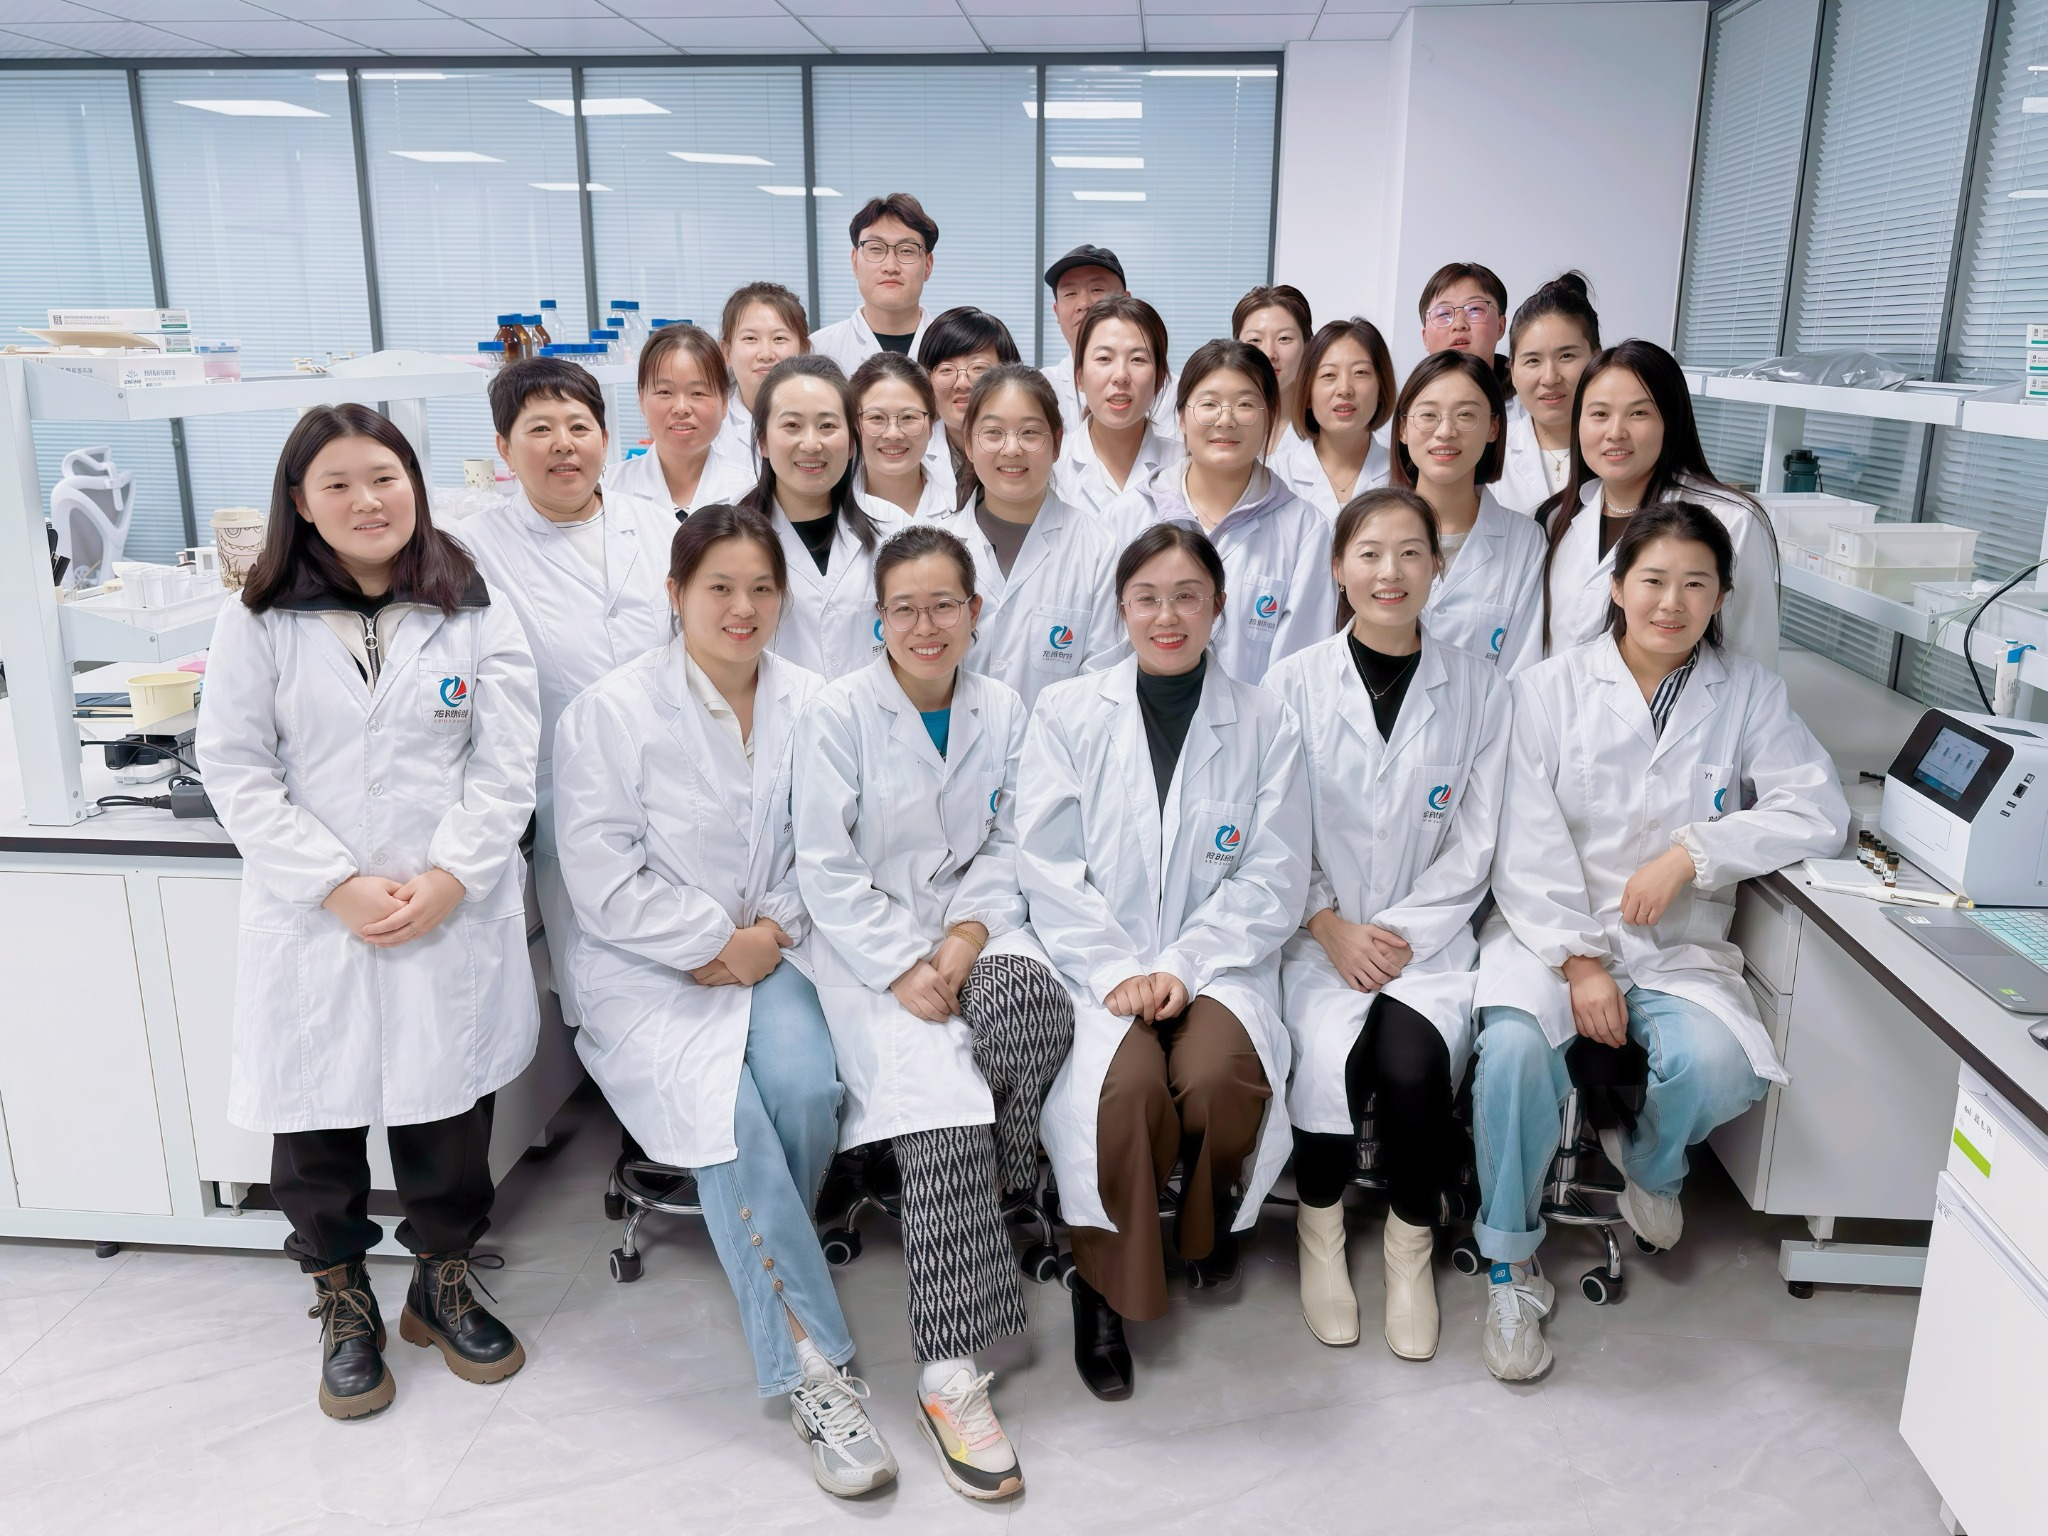
Expertise across veterinary medicine, microbiology, pharmacology, chemistry, immunology and molecular biology supports the development of assays and systems for complex real-world applications.
Core reagents and assay development across fluorescence immunoassay, ELISA, colloidal gold and related technologies.
Integrated instrument, incubation, reading, sample preparation and automated testing workflow development.
Matrix-specific extraction, range, recovery, precision and routine workflow evaluation for practical use.
Batch consistency, product release, method setup, training, troubleshooting and ongoing application support.
Our Focus Areas
Four business areas supported by shared scientific, manufacturing and automation capabilities.
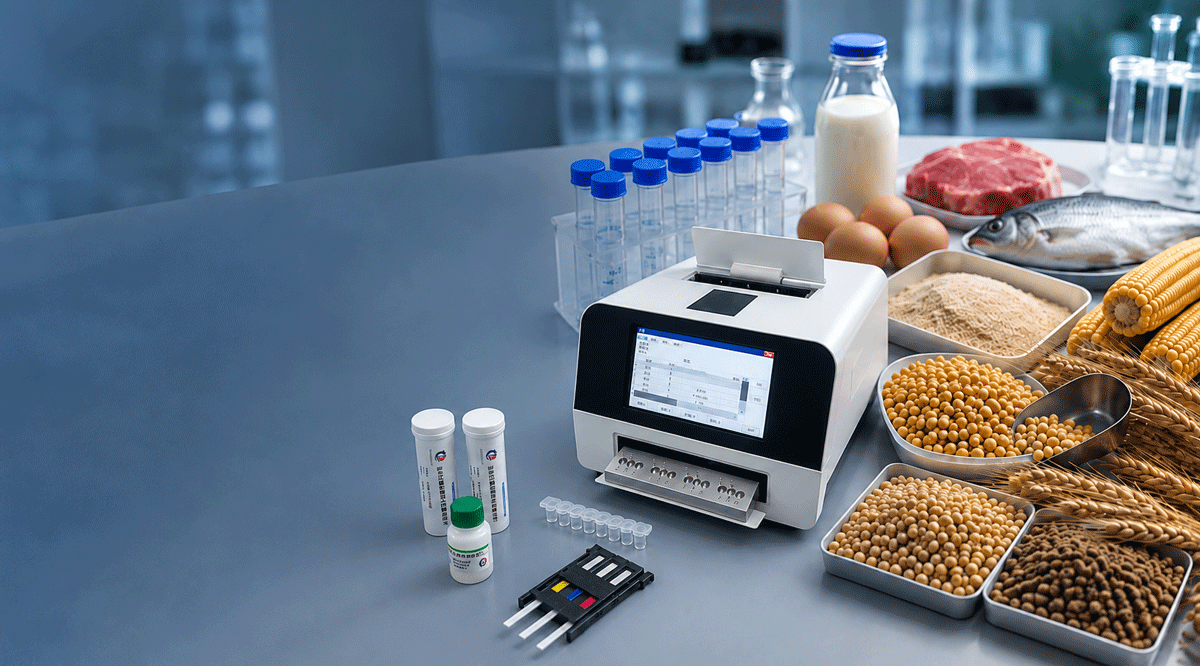
Rapid and laboratory-based solutions for routine contaminant and residue monitoring across raw materials, processing and finished products.

Specialized ELISA solutions supporting raw material evaluation and processing effectiveness.

Molecular diagnostic solutions for pathogen detection, disease monitoring and biosecurity management.

Coordinated systems covering sample preparation, rapid screening, detection and data workflows to improve consistency and throughput.
Integrated R&D & Manufacturing
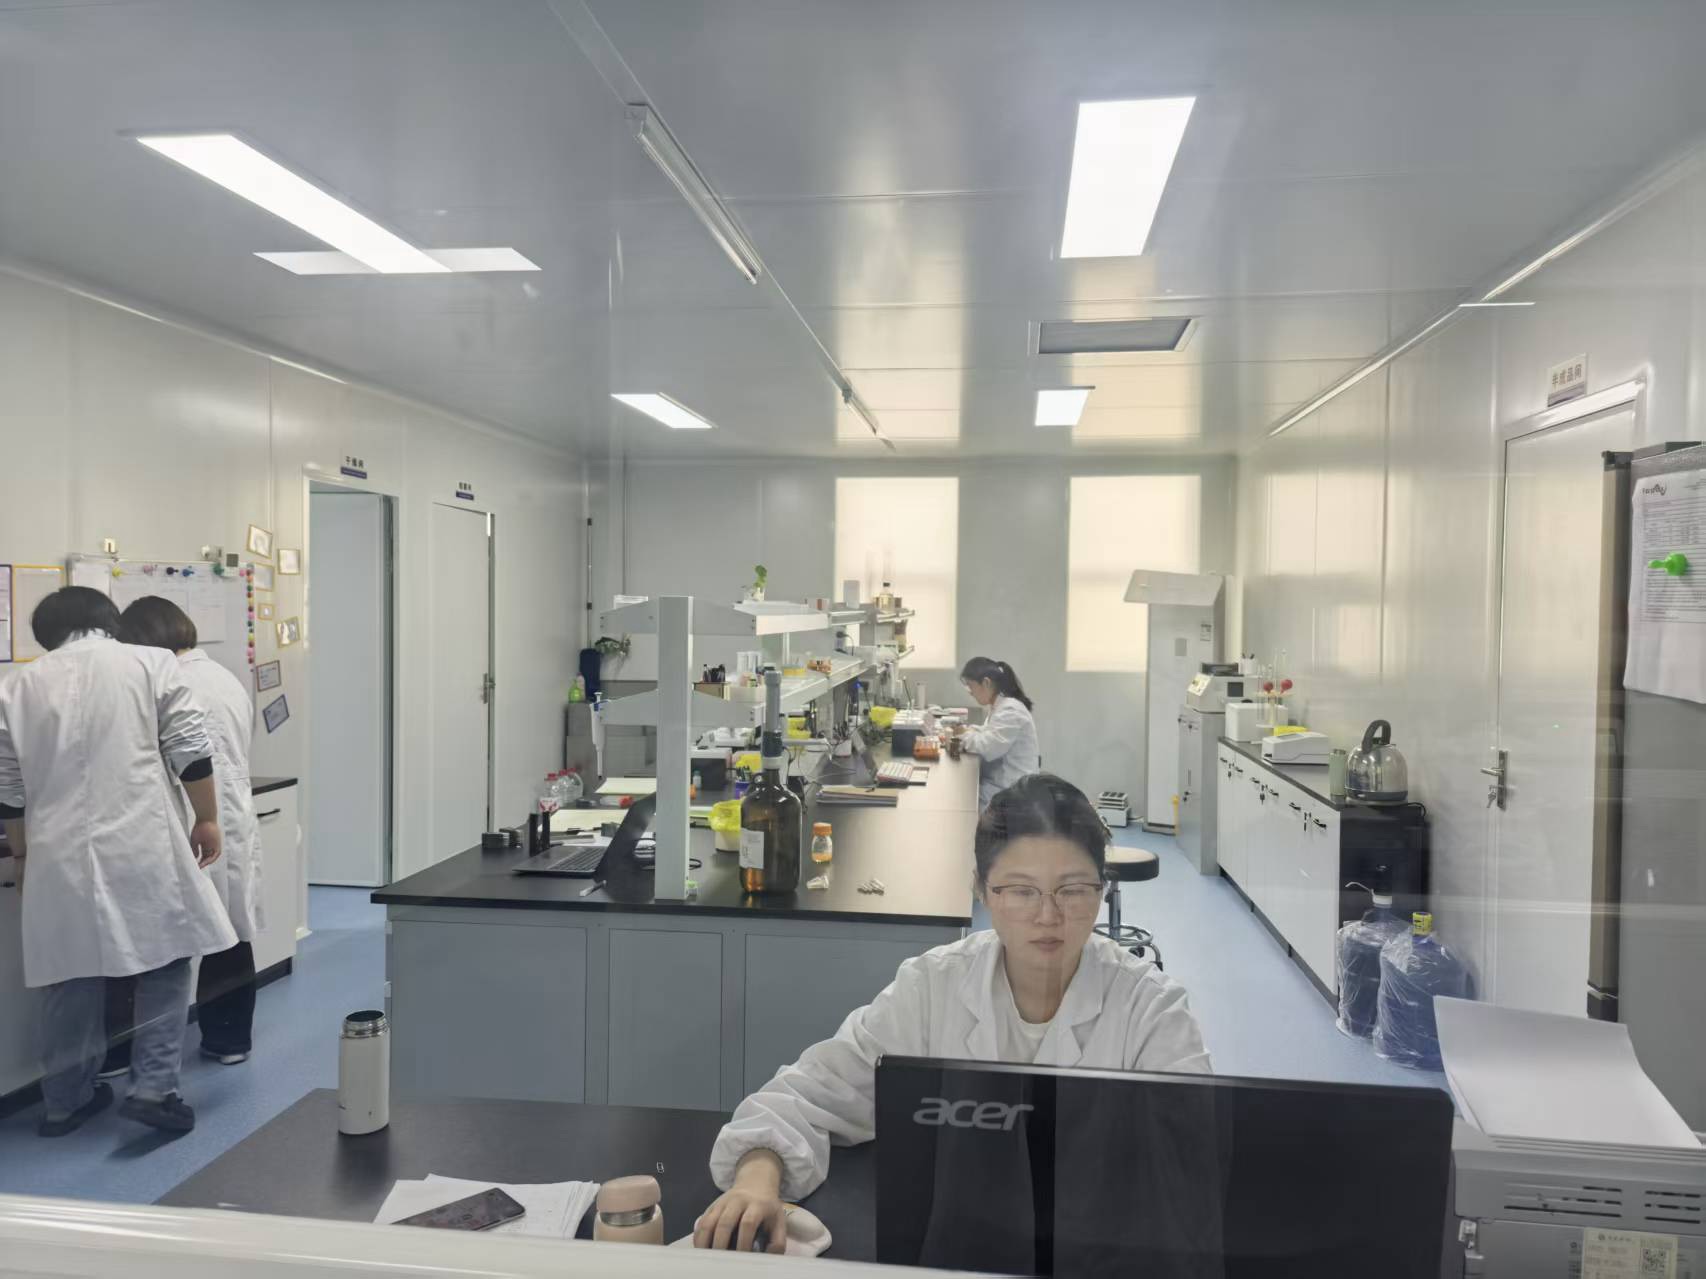
Xinyu Bio connects core reagent preparation, assay design, performance validation, automated manufacturing, in-process control and final release—turning laboratory concepts into repeatable products for routine testing.
 Scientific Development
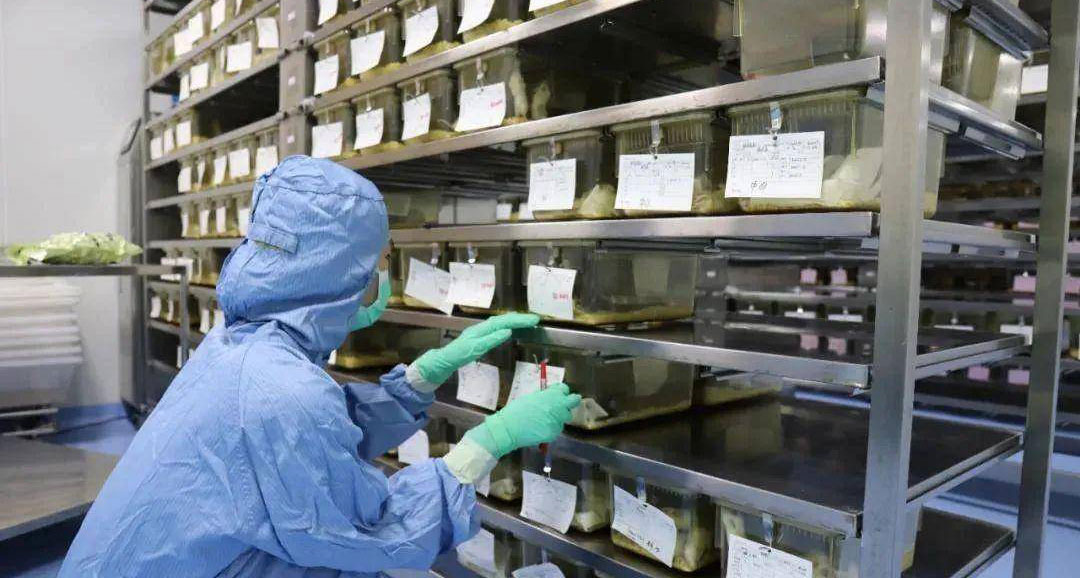 Core Reagent Preparation
Our multidisciplinary team develops core reagents, assay chemistry, sample preparation methods and instrument-matched workflows, then evaluates performance across target ranges and representative sample matrices.
Validated designs are transferred into standardized production steps, with automated equipment applied where precision, repeatability and traceability matter.
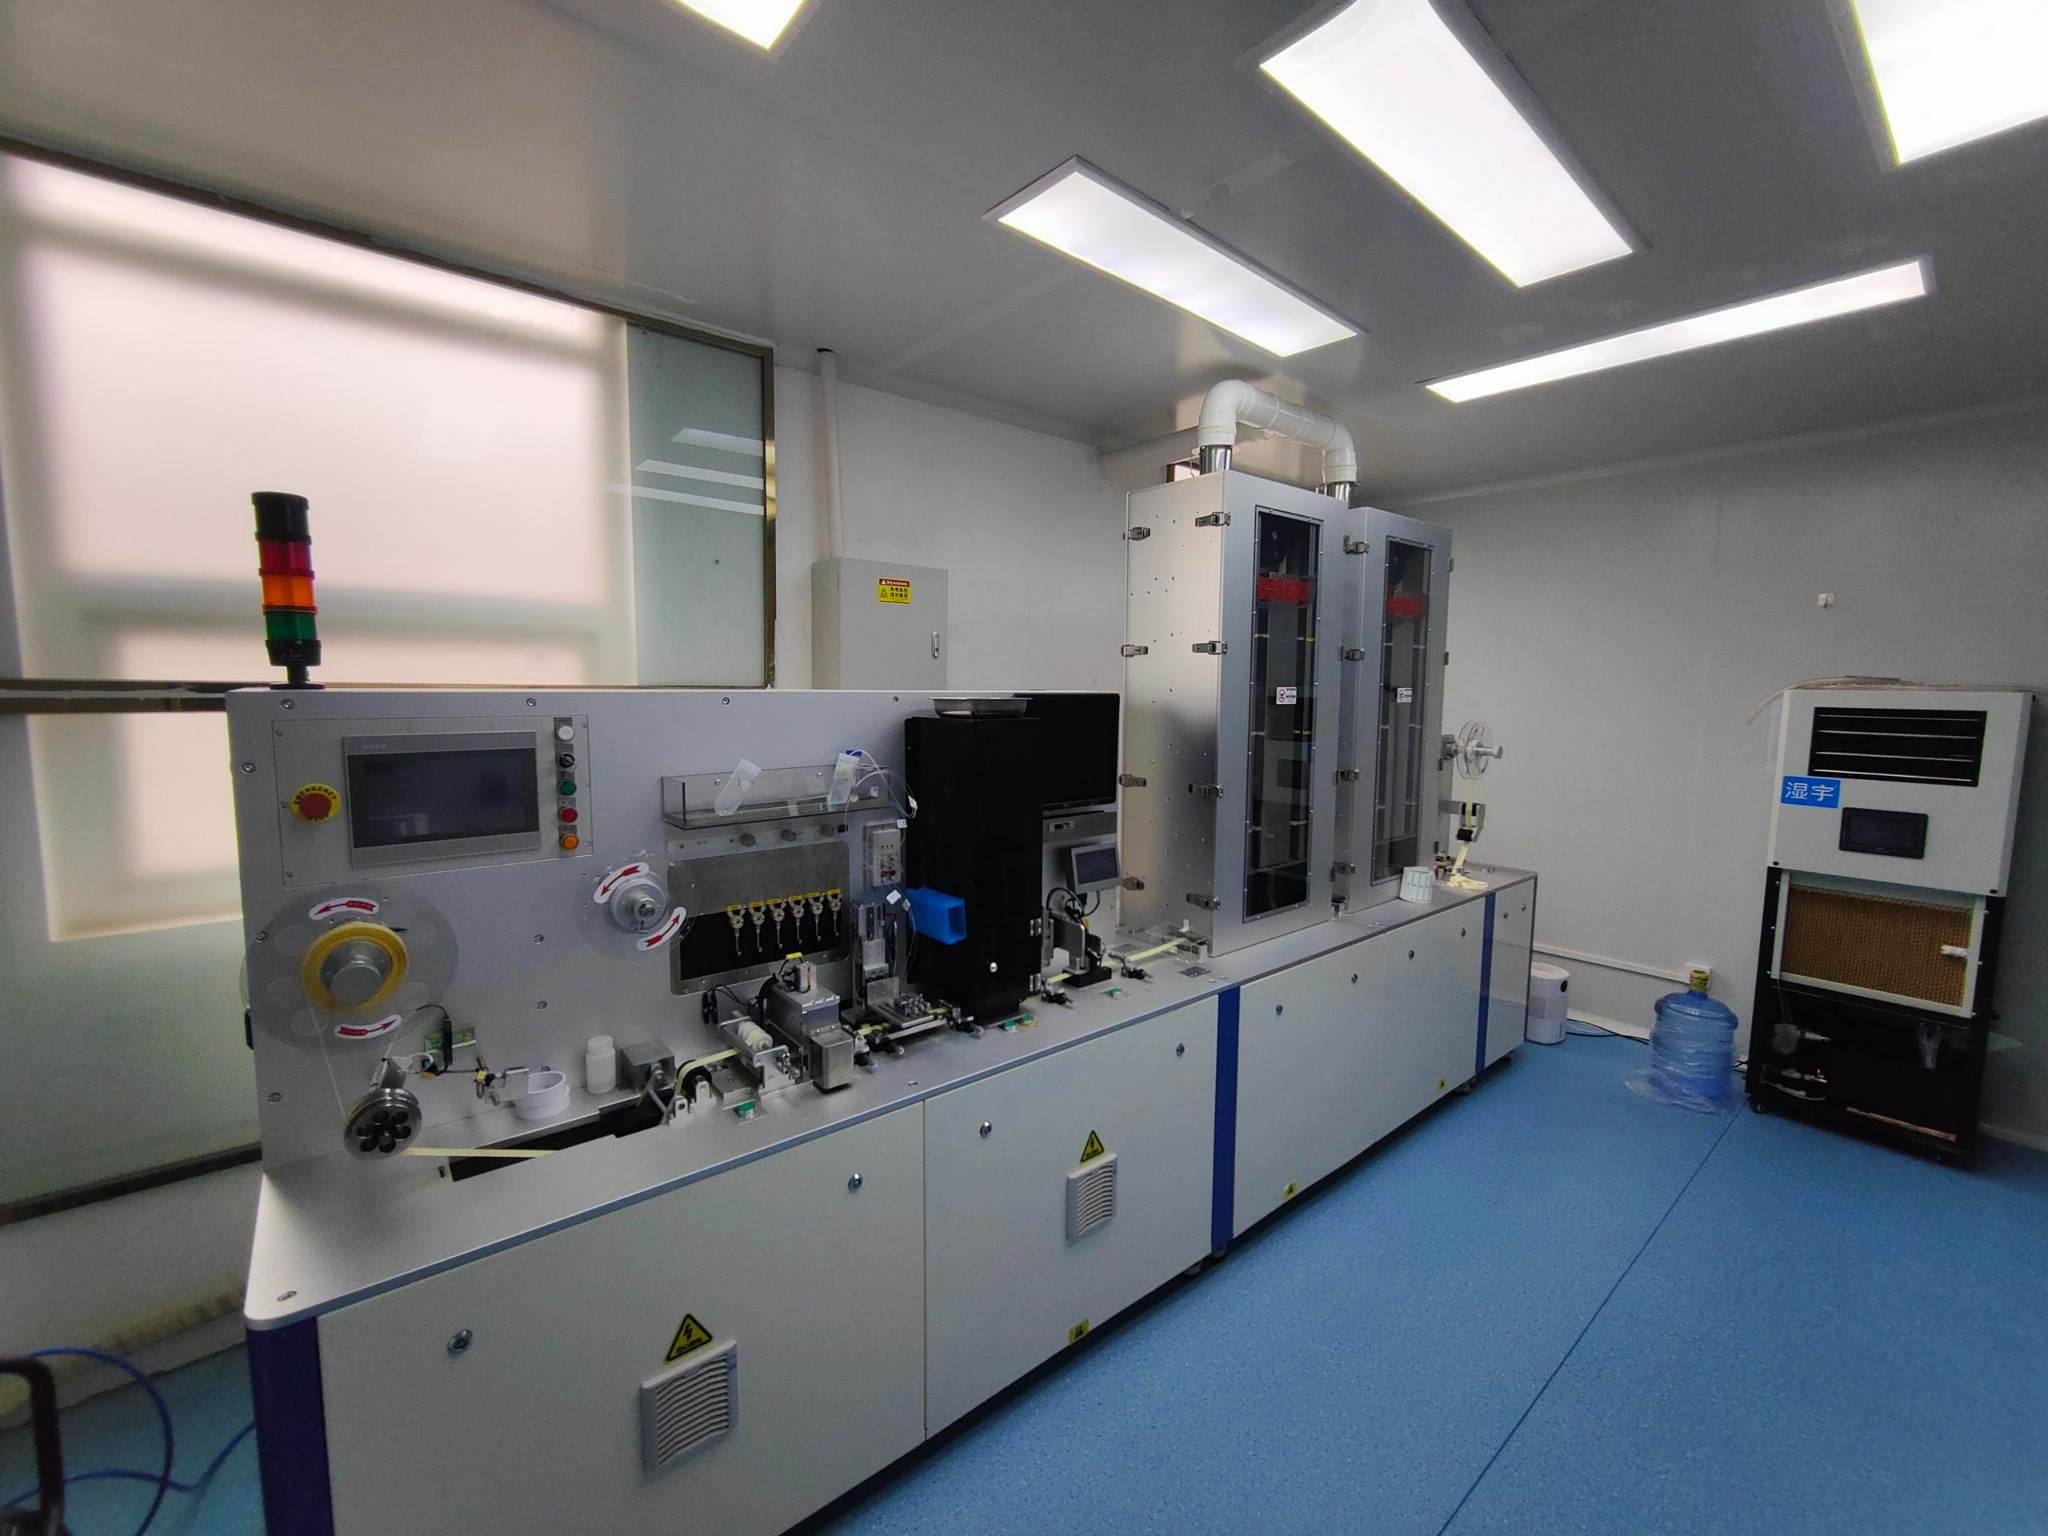 Stage 02
Controlled dispensing and membrane processing support consistent quantitative rapid-test strip production.
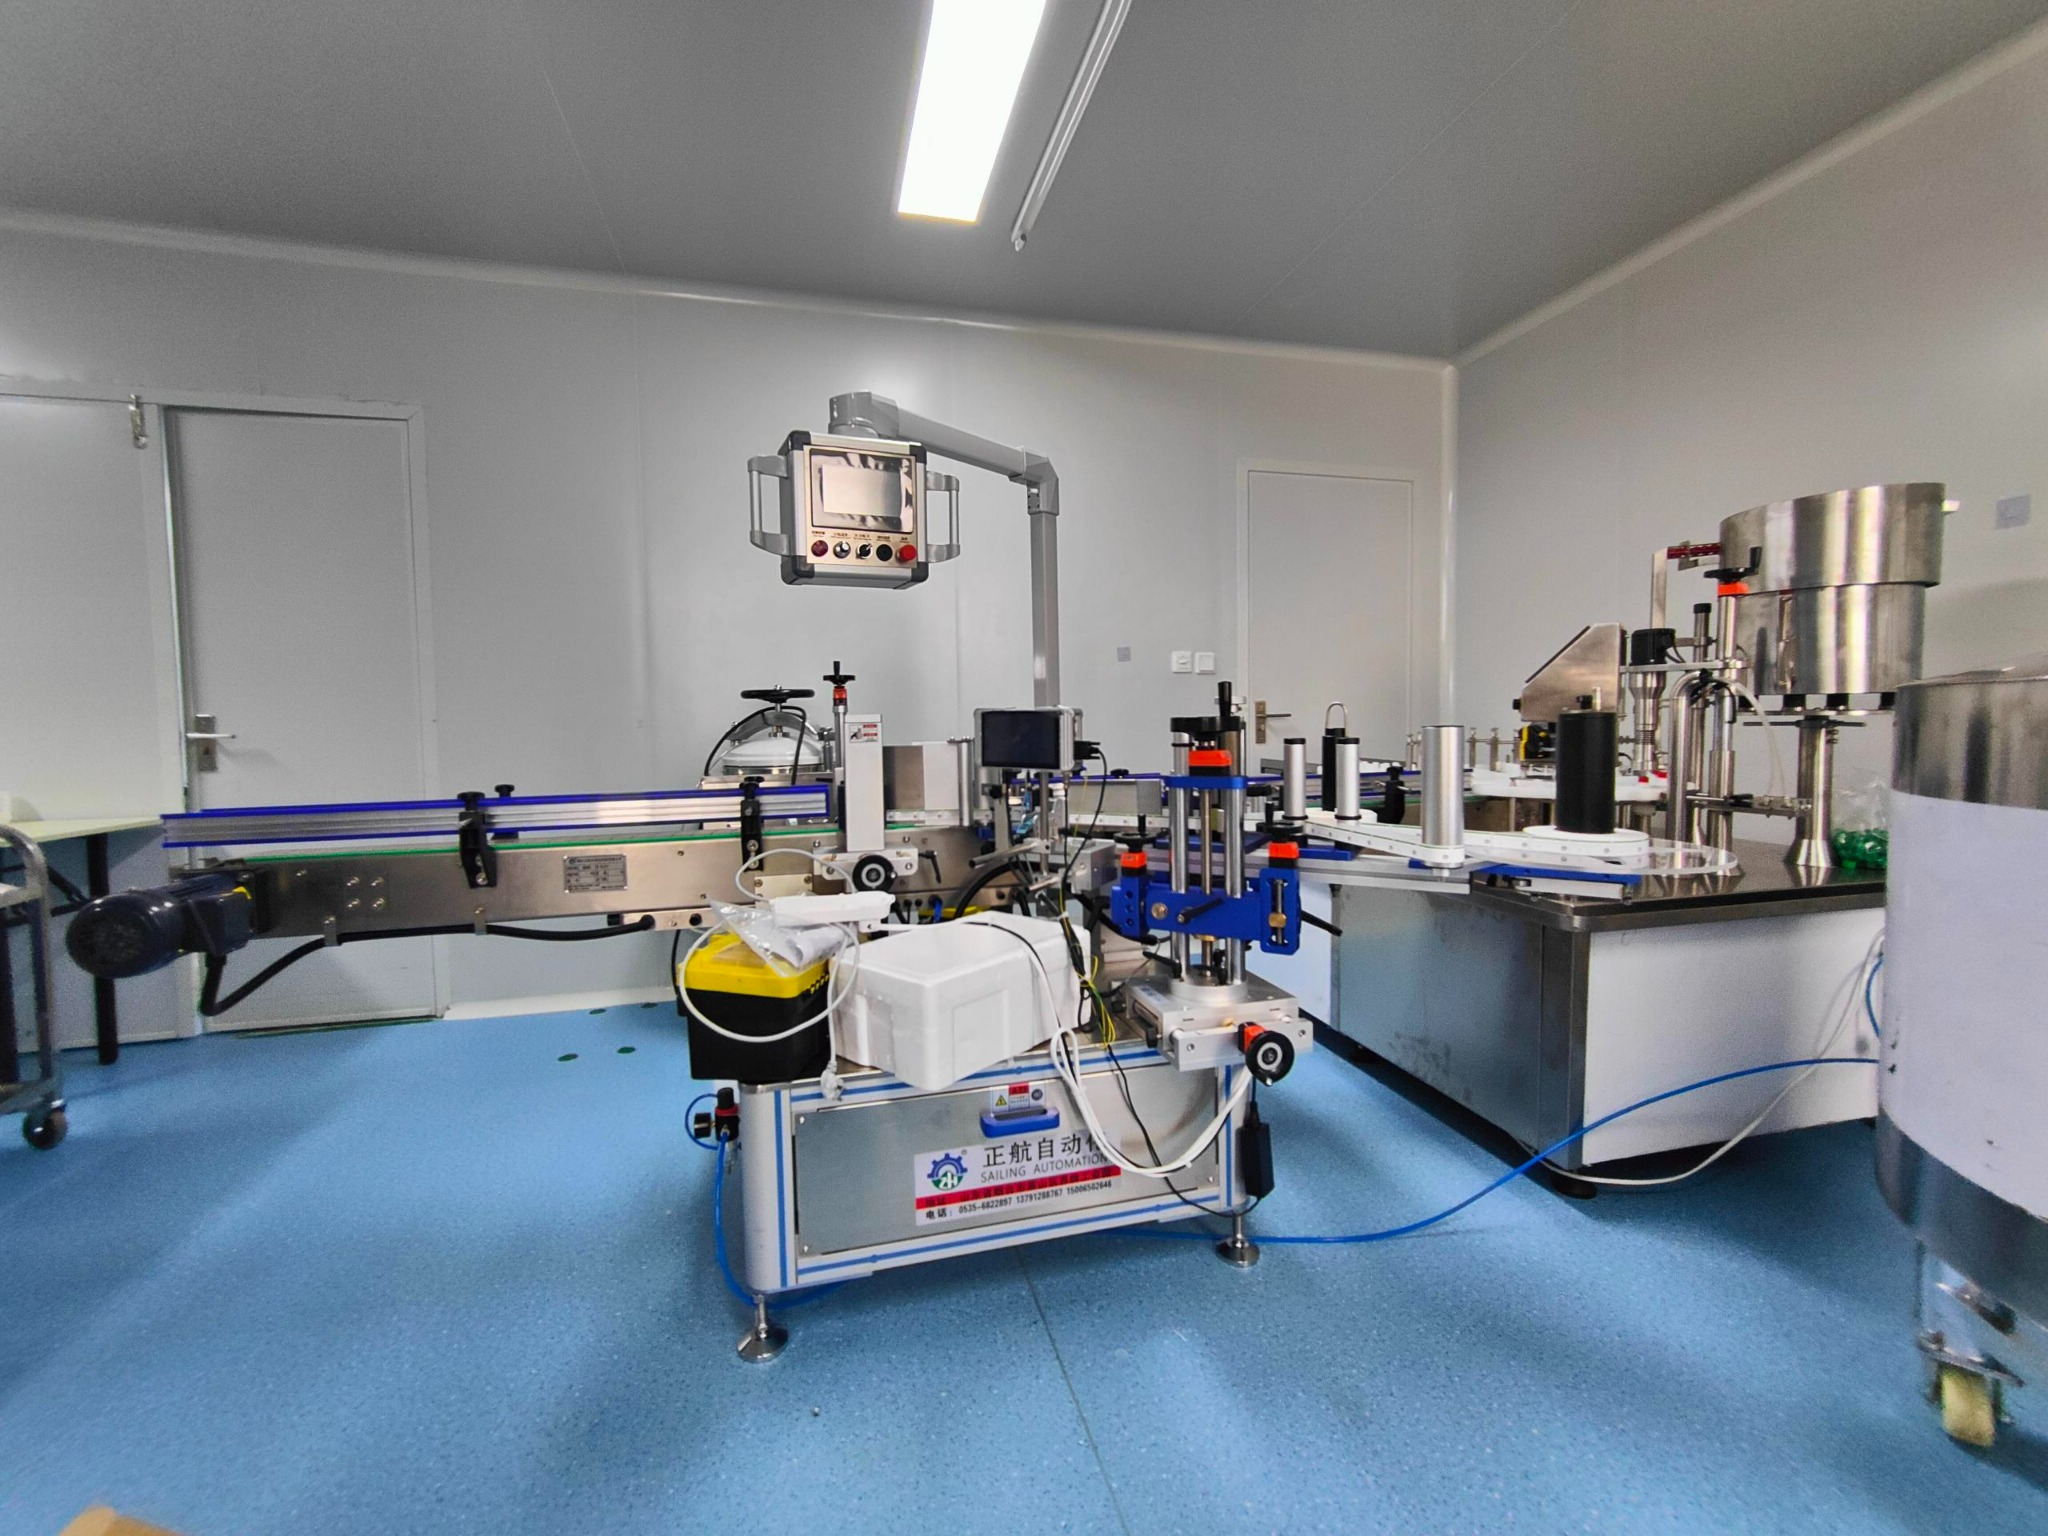 Stage 03
Automated filling and labeling improve process consistency, packaging traceability and production efficiency.
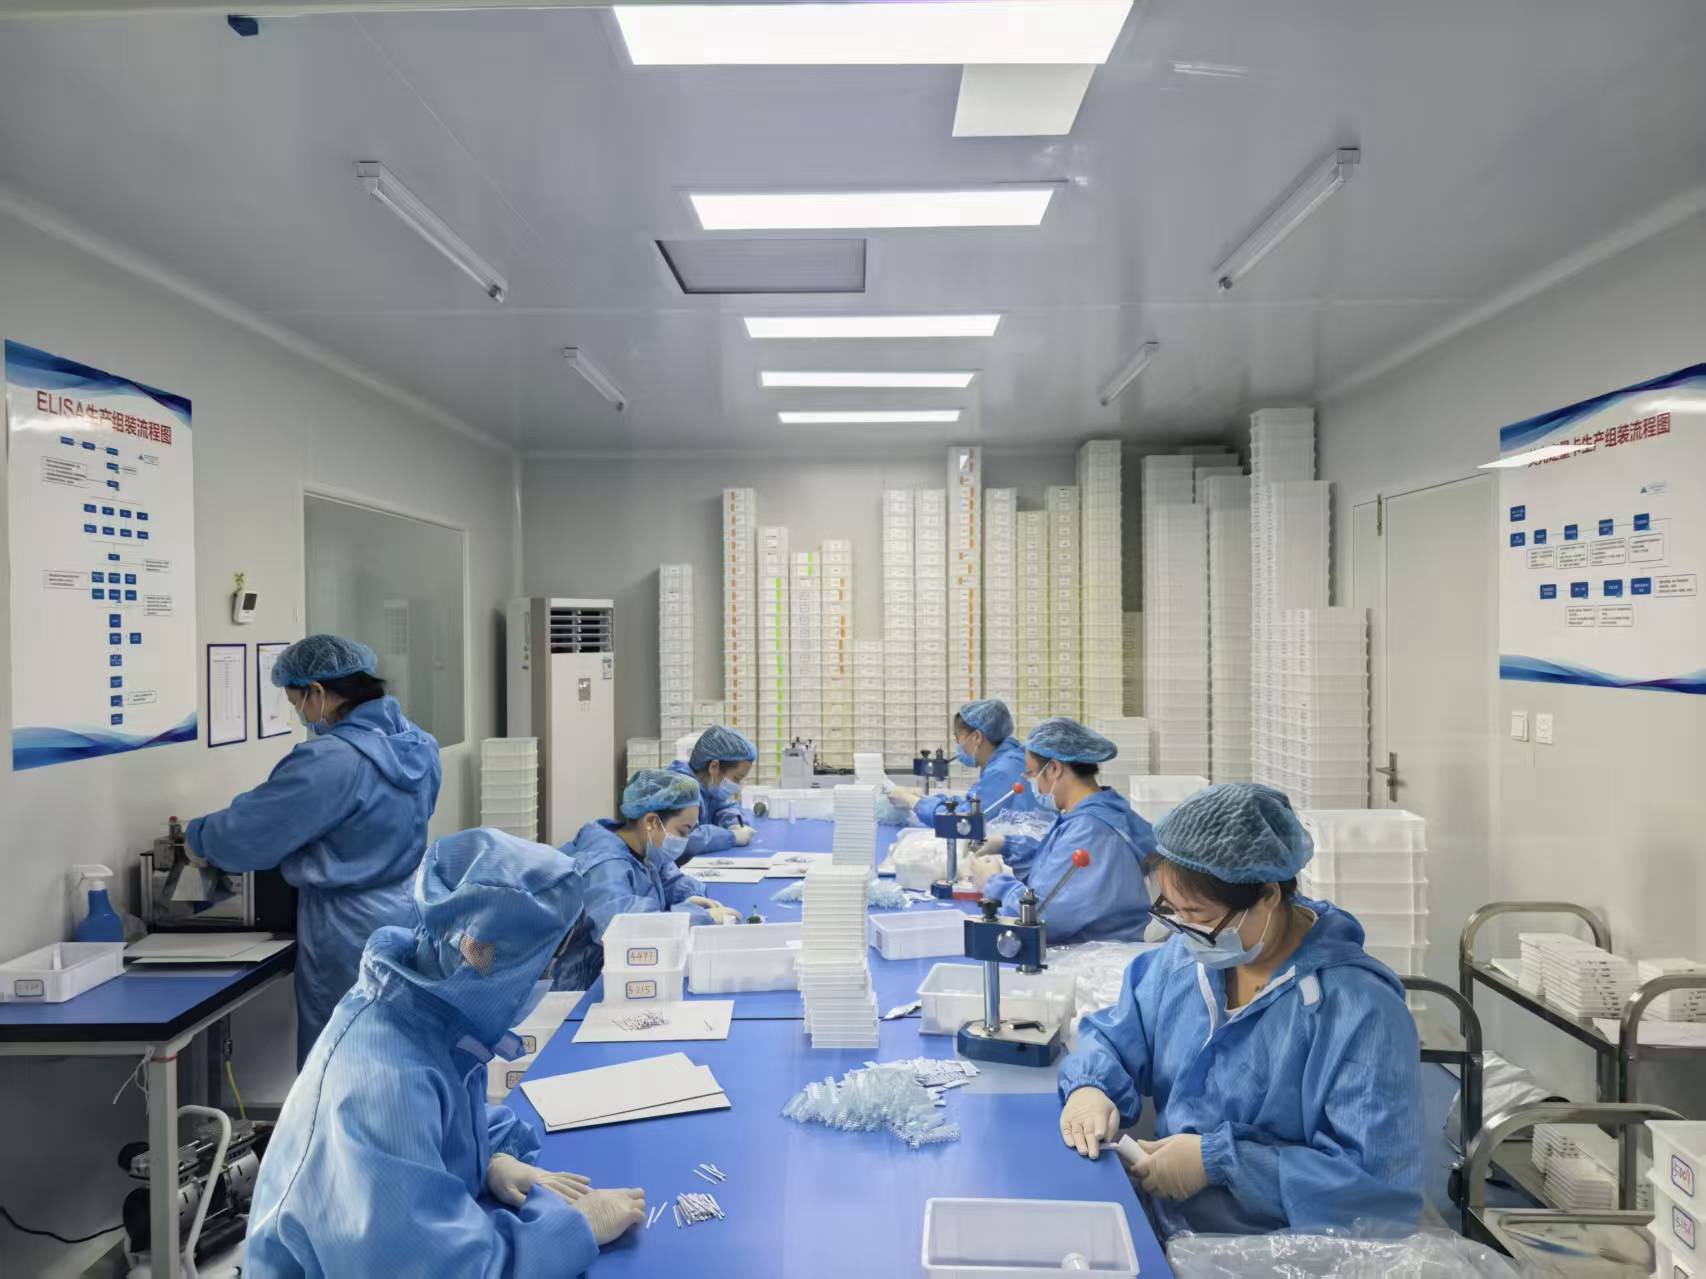 Stage 04
Controlled assembly, in-process inspection and final packaging complete the workflow before batch release and shipment.
Our Journey
From feed safety assays to integrated diagnostics and intelligent automation.
Mycotoxin rapid tests and ELISA technologies for complex feed matrices.
Introduced dedicated tests for soybean anti-nutritional factors.
Quantitative mycotoxin rapid tests with coordinated sample preparation.
Expanded fluorescence quantitative testing across food and feed matrices.
Expanded into veterinary drug residues, pesticide residues and other risks.
Developed integrated and automated testing platforms.
Completed a sub-project under China’s 14th Five-Year Plan National Key R&D Program.
Trusted Across Industries
Xinyu Bio technologies support routine quality control across feed and animal nutrition, grain and edible oil, food processing and animal-derived food production. The companies below represent a selection of long-term and application-focused collaborations.
Companies served with mycotoxin rapid testing solutions
Estimated annual value protected through mycotoxin risk control*
Estimated annual value protected through soybean ANF quality control*
Rapid screening helps customers identify high-risk raw materials before production, reducing batch rejection and downstream losses associated with excessive mycotoxin levels.
ELISA testing supports incoming quality control of soybean meal and processed soy ingredients, helping feed producers evaluate raw-material quality and reduce losses associated with excessive anti-nutritional factors.
*Estimated from customer application scenarios and Xinyu Bio’s internal economic model. Actual impact may vary depending on material prices, testing volume, production conditions and quality-control practices.
A selection of customers and industry partners using Xinyu Bio products, instruments and application workflows.
Why Xinyu Bio
Three principles guide how we develop every product and solution—from assay chemistry and instrument engineering to routine application.
Intelligent & Automated
Xinyu Bio independently develops and manufactures intelligent instruments and automated testing systems, matching reagents, equipment and workflows for efficient operation and dependable results.
Accuracy You Can Trust
In food-safety testing, accuracy is the foundation of every quality-control decision. Long-term service to major industry groups and testing laboratories demonstrates the consistency and dependability of our products in routine use.
Continuous Innovation
Across the food-safety testing chain, we continually improve operating experience, detection principles, intelligent instruments and the relevance of testing indicators—translating new ideas into practical products and solutions.
Whether you need rapid screening, laboratory testing or automated workflows, our team can help evaluate your requirements and recommend a practical approach.